Key Takeaways
- Semaglutide's amino acid chain runs 31 residues, longer than most legacy peptide drugs, raising the bar for impurity control.
- Commercial-scale GLP-1 peptide manufacturing typically combines SPPS for chain assembly and LPPS for fragment coupling.
- Validated batch performance at full commercial volume separates large-scale peptide CDMOs from clinical-stage providers.
- Evaluating a peptide CDMO for GLP-1 manufacturing comes down to five factors: GMP certification, reactor capacity, commercial-scale production history, regulatory filing experience, and written lead-time commitments.
- Neuland runs SPPS reactors up to 750L and LPPS reactors from 250L to 6,250L under FDA, EMA, and PMDA-approved cGMP standards, with a new Bonthapally facility module adding 6,370L of capacity by late 2026.
GLP-1 peptides require production volumes far beyond typical peptide drugs, often reaching multi-ton annual output. Most existing peptide manufacturing capacity was built for smaller programs. When GLP-1 demand climbed, many manufacturers found their reactor capacity too small to keep pace.
Adding new capacity for GMP peptide manufacturing takes years, covering construction and regulatory qualification alike. That timeline pushes most companies toward an established peptide CDMO instead of building new capacity in-house. The right partner, therefore, already holds GMP certification and reactor capacity sized for commercial GLP-1 batches.
Understanding GMP Peptide Manufacturing for GLP-1 APIs
GMP peptide manufacturing is the production of peptide active pharmaceutical ingredients under current Good Manufacturing Practice standards. Regulators such as the FDA and EMA enforce these standards, along with Japan's PMDA. The rules govern how a peptide is synthesized. They also govern purification and the testing performed before release.
GLP-1 peptides carry longer amino acid sequences than most legacy peptide drugs. For example, semaglutide's chain contains 31 amino acids. Sequences at this length are harder to purify cleanly. That difficulty raises the bar for impurity control at every batch.
Two synthesis methods handle this complexity. SPPS (solid-phase peptide synthesis) builds the chain one amino acid at a time on a resin support. LPPS (liquid-phase peptide synthesis) assembles shorter fragments in solution before they are joined to form the full sequence. Commercial-scale GLP-1 production often uses both methods together.
A peptide CDMO manages this process under one quality system, from synthesis through analytical release testing. That continuity keeps impurity data and batch records consistent as a molecule moves from development into commercial output.
How Do You Evaluate a Peptide CDMO for GLP-1 Manufacturing?
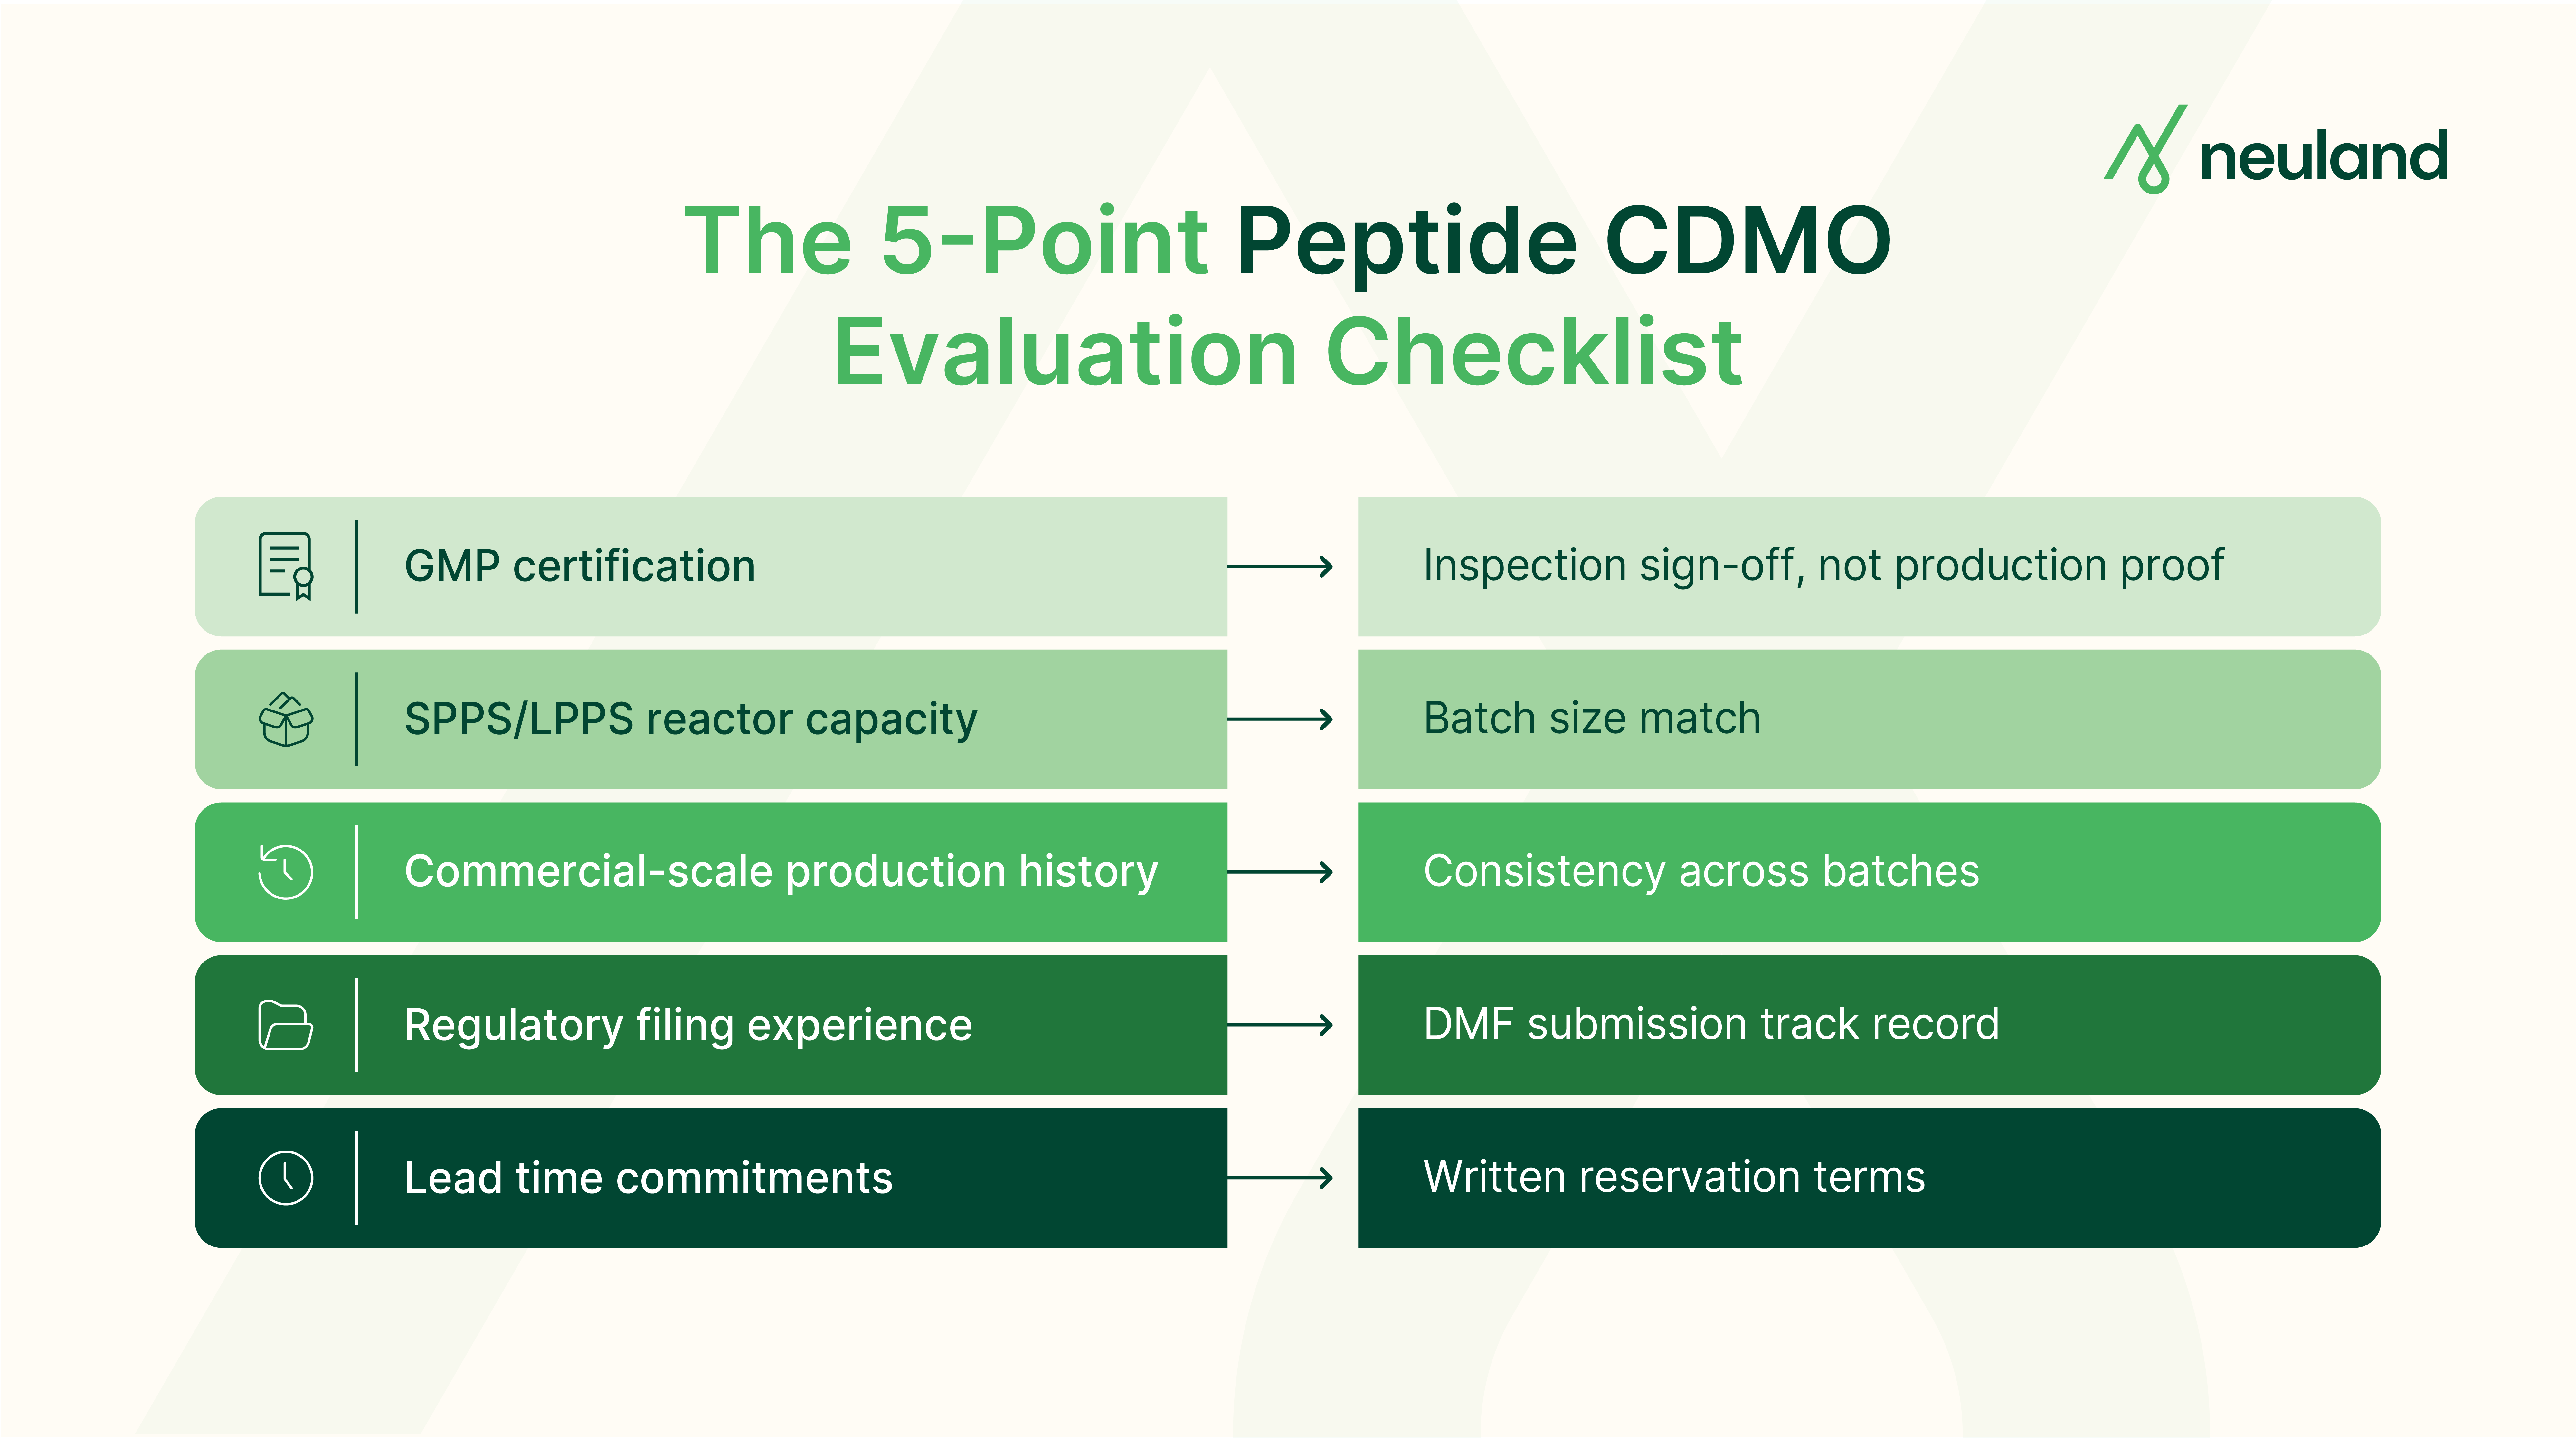
Evaluating a peptide CDMO means checking five specific areas before committing to one. Here are the criteria that matter most for GLP-1 peptide manufacturing, and what each one confirms:
- GMP certification
It confirms that the facility has passed inspections by regulators such as the FDA, the EMA, and Japan's PMDA. Certification covers quality systems and documentation control, along with environmental monitoring. It does not confirm that the facility has previously produced a GLP-1 peptide at commercial scale. - SPPS and LPPS reactor capacity
This determines the batch size a CDMO can deliver. Clinical-stage supply needs a multi-kilogram reactor volume. Commercial GLP-1 batches need reactor capacity in the hundreds or thousands of liters. Match the reactor size to your target volume rather than the largest figure on a capabilities sheet. - Commercial-scale production history
It shows whether a CDMO has run batches at the volume your project needs, and not merely at pilot scale. Ask for yield and purity data across several past batches. A single reference run does not prove consistency. - Regulatory filing experience
It confirms the CDMO has supported drug master file submissions for prior molecules. That experience means the provider understands what regulators expect in a GLP-1 filing package. It also tends to shorten review cycles. - Lead time commitments
This last criterion protects your launch schedule. Ask for reservation terms in writing rather than a verbal estimate. Commercial-scale GLP-1 slots often book out months ahead, so a written commitment prevents last-minute capacity conflicts.
Weigh these five areas together. A peptide CDMO with certification but no matching reactor capacity cannot support commercial GLP-1 volumes. One with reactor capacity but no filing history adds regulatory risk instead.
Who Can Scale Up GLP-1 Peptide Manufacturing?
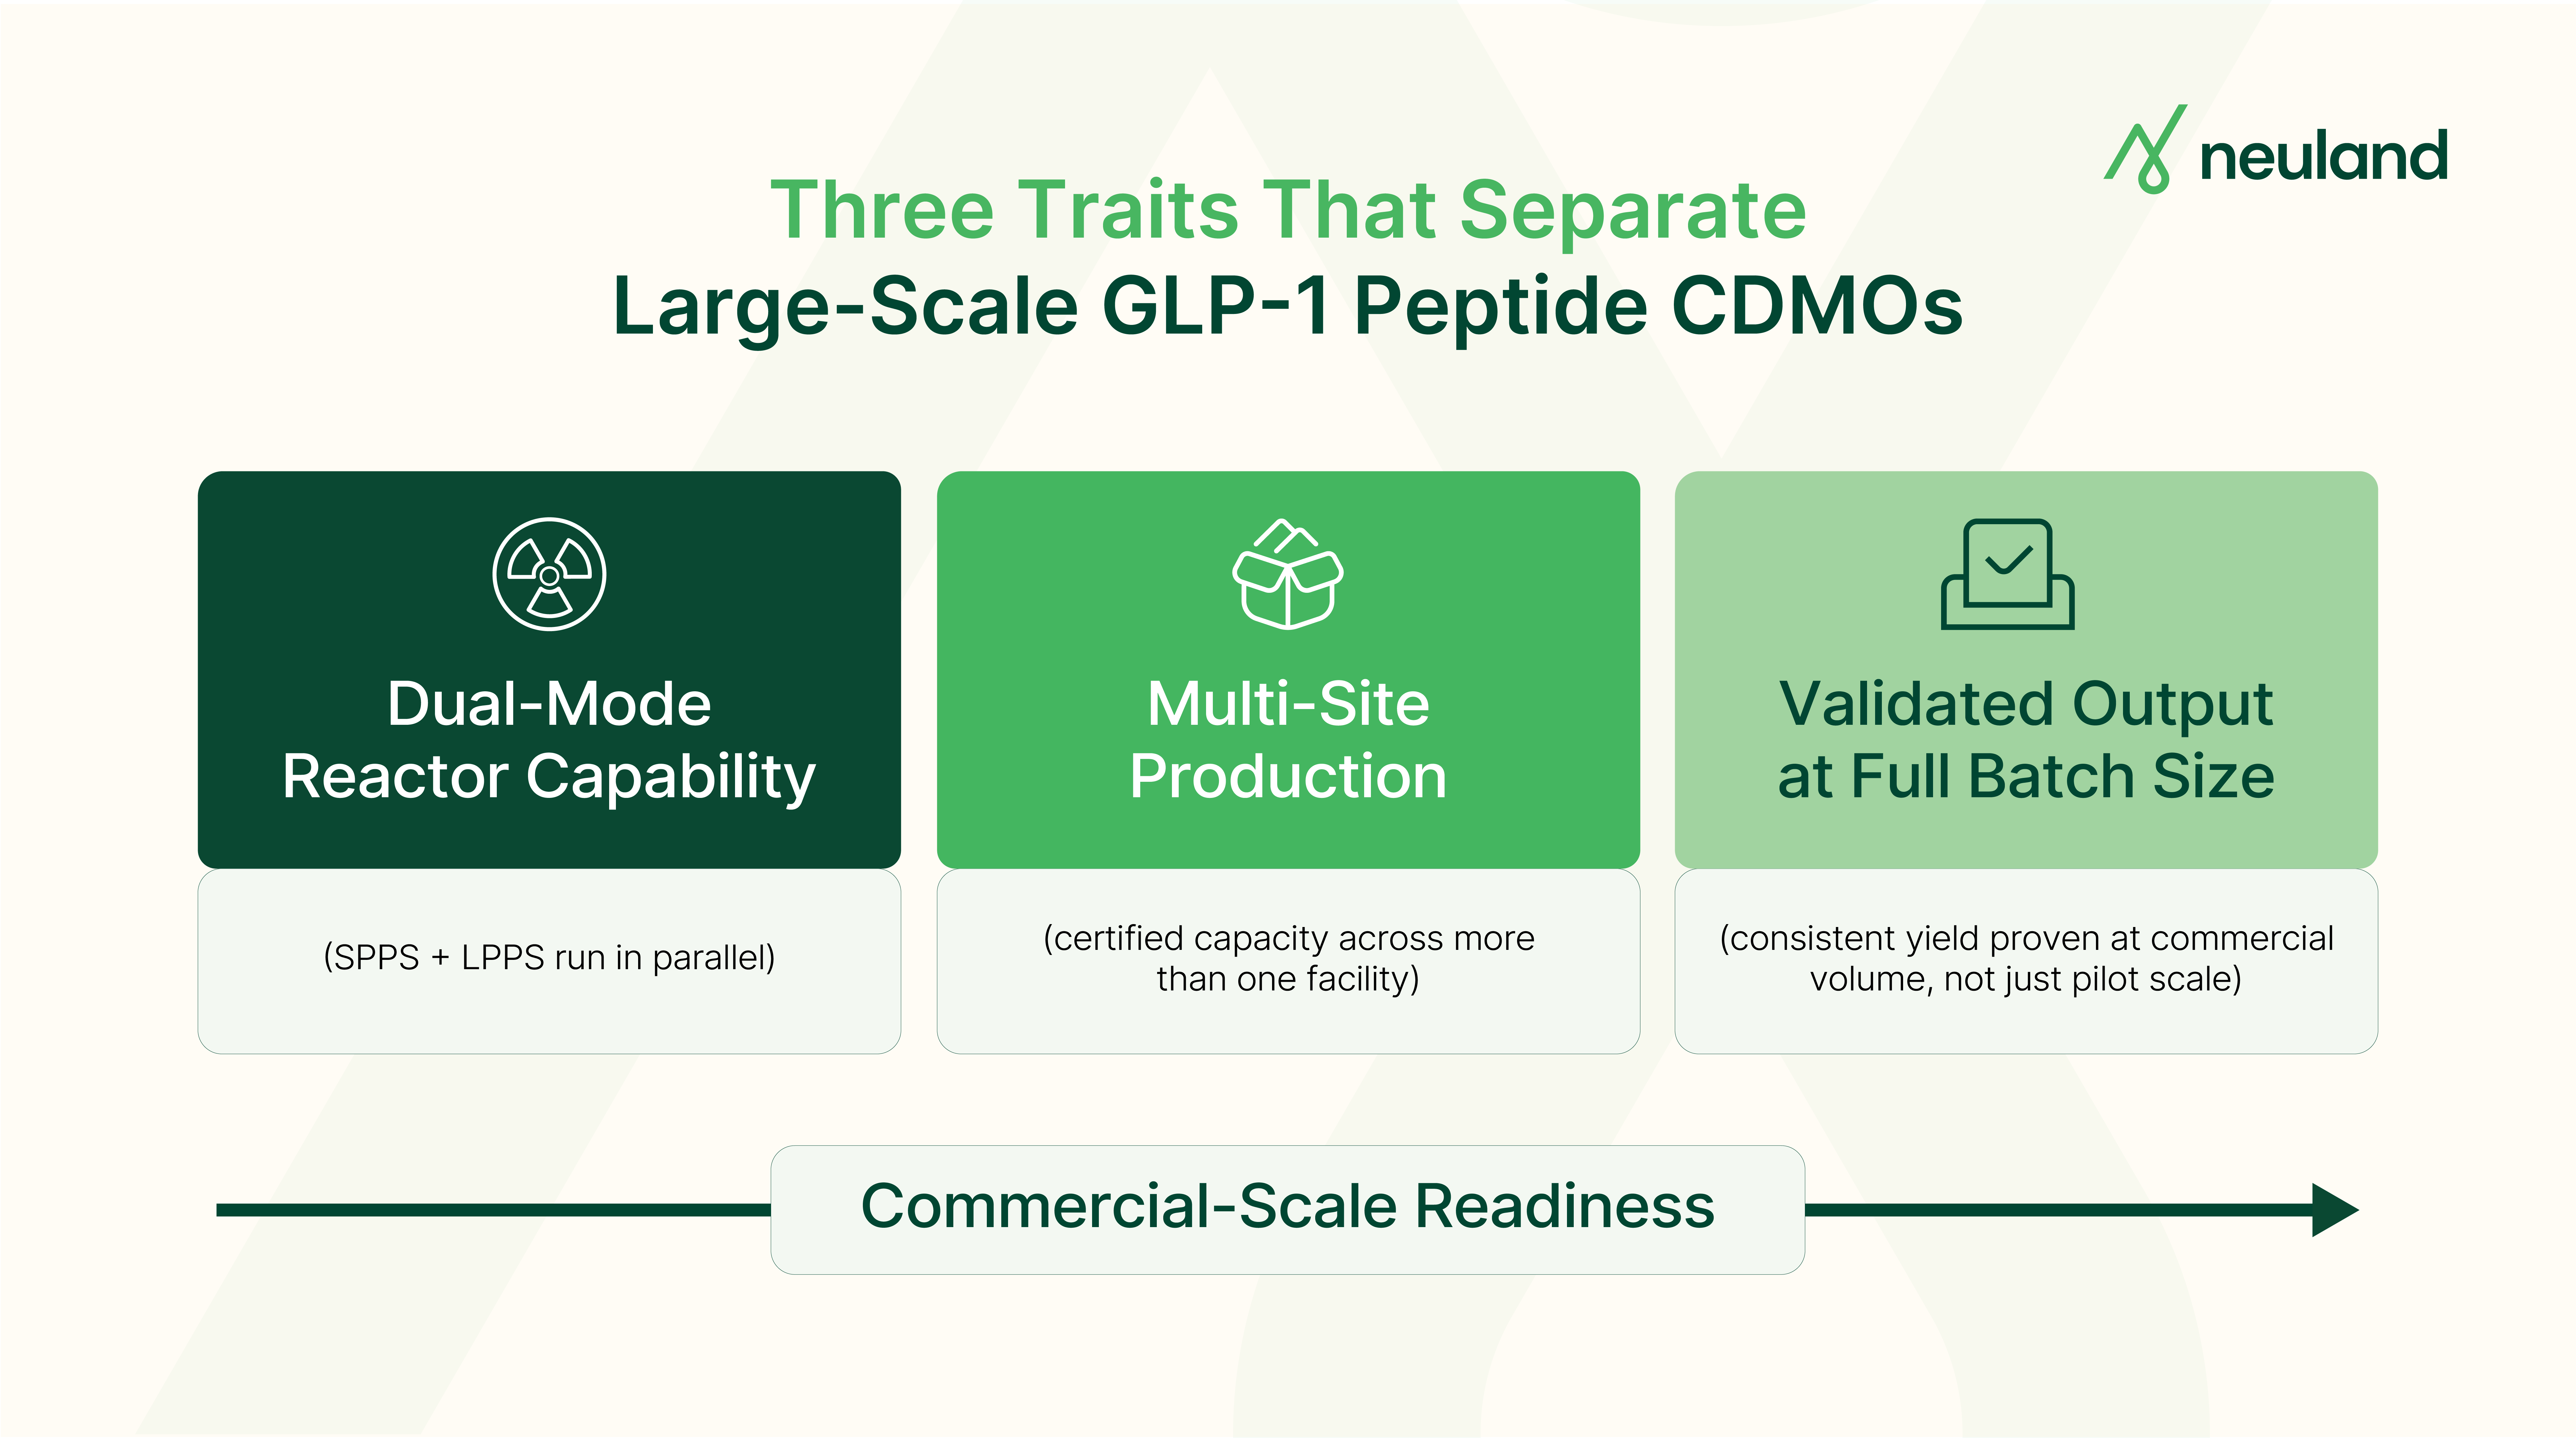
A small group of CDMOs can scale GLP-1 peptide manufacturing to commercial volume. Batch performance at full scale is what separates them, more than certification alone.
- Dual-mode reactor capability: GLP-1 peptides typically need SPPS for chain assembly and LPPS for fragment coupling. A peptide CDMO running both lines in parallel can move a batch through both stages without transferring it to a second facility.
- Multi-site production: Certified capacity spread across more than one facility protects a continuous supply. A delay at one site does not stall the full order.
- Validated output at full batch size: A reactor rated for 2,000L does not guarantee a consistent yield at that volume. Providers that scale successfully have validated their process at a commercial batch size, rather than only at pilot scale.
The FDA's February 2025 resolution of the semaglutide shortage shows why this distinction matters. The shortage began in 2022, when demand outpaced available supply. It closed once the manufacturer confirmed its production capacity could reliably meet current and projected demand at full commercial volume. Certification had already been in place for years before that point. The shortage ended when validated capacity caught up to it.
Which Peptide CDMOs Have Large-Scale cGMP Capacity?
Peptide CDMOs with large-scale cGMP capacity share three traits: commercial-scale reactor volume, consistent batch yield at that volume, and cGMP certification tied to a proven production history.
Reactor volume is the first marker. A peptide CDMO that runs only clinical-stage reactors produces gram- to single-digit-kilogram batches. It is enough for a trial supply but not for a launched GLP-1 drug. A CDMO with large-scale capacity operates reactors built for multi-kilogram and multi-ton output instead.
| Capability | Clinical-Stage CDMO | Large-Scale CDMO |
|---|---|---|
| Typical batch output | Grams to a few kilograms | Multi-kilogram to multi-ton |
| Reactor design | Sized for trial supply | Sized for national or global commercial demand |
| Production history | Limited or early-stage | Documented commercial batches |
Reactor size by itself doesn't confirm capacity. A peptide CDMO with large-scale capacity also holds consistent yield and purity across every batch it runs at that volume.
Certification narrows the field further. It doesn't confirm experience in commercial-scale production. Only CDMOs that combine certification with documented large-volume output qualify as having true large-scale cGMP capacity.
What Are Neuland's GLP-1 Peptide Manufacturing Capabilities?
Neuland manufactures GLP-1 peptides through SPPS and LPPS. It operates under cGMP standards and holds approvals from the FDA, EMA, and Japan's PMDA. Current SPPS reactors run up to 500L, while LPPS reactors span 250L to 3,000L, sized for multi-kilogram output. Data integrity across both lines follows 21 CFR Part 11, backed by DCS-based automation.
Neuland's existing SPPS and LPPS capacity is scaled further by a new commercial peptide facility at its Bonthapally campus near Hyderabad. This facility adds 6,370L of combined SPPS and LPPS reactor capacity.
This combination matters for buyers evaluating a CDMO today. Current SPPS and LPPS capacity supports near-term GLP-1 programs. The new facility adds a path to larger commercial volumes.
Summary
- GMP peptide manufacturing depends on cGMP certification, validated reactor capacity, and documented production history together.
- SPPS and LPPS remain the two production methods behind commercial GLP-1 peptides, often used together.
- Reactor capacity and production history are what separate large-scale peptide CDMOs from providers still working at clinical-stage volume.
- Neuland combines existing SPPS and LPPS capacity with an expanding Bonthapally facility, giving buyers a path from near-term GLP-1 supply to larger commercial volume.
Planning your next step with a peptide CDMO?
Neuland assigns a dedicated project team to each molecule, carrying forward batch and process knowledge as the program moves toward commercial scale. Analytical release testing runs alongside manufacturing under the same quality system. Connect with Neuland's peptide team to discuss your project's next stage.
FAQs
Lead time for peptide manufacturing capacity varies with batch size and reactor availability. It also depends on the facility booking schedules. Commercial-scale slots for high-demand molecules like peptides often fill months ahead of the intended production date. Confirming a reservation window early, before committing to a launch timeline, avoids capacity gaps later.
GMP peptide manufacturing at commercial scale is offered by CDMOs holding current cGMP certification from regulators like the FDA, EMA, and Japan's PMDA. These providers combine SPPS and LPPS reactor lines with a documented history of commercial batch production.
Yes, Neuland supports both clinical-stage and commercial-scale peptide manufacturing within the same facilities. This means a molecule can move from early development through launch volume without changing providers. You can explore Neuland's peptide services to see how this applies to a specific molecule.
Demand for peptide CDMO capacity has increased as GLP-1 prescribing volumes have grown quickly across multiple therapeutic uses. Manufacturing capacity takes years to build, while patient demand can shift within months. That mismatch keeps commercial-scale peptide CDMO slots in short supply.