
Purpose-built for complex peptide chemistry, controlled scale-up, and reliable commercial supply.
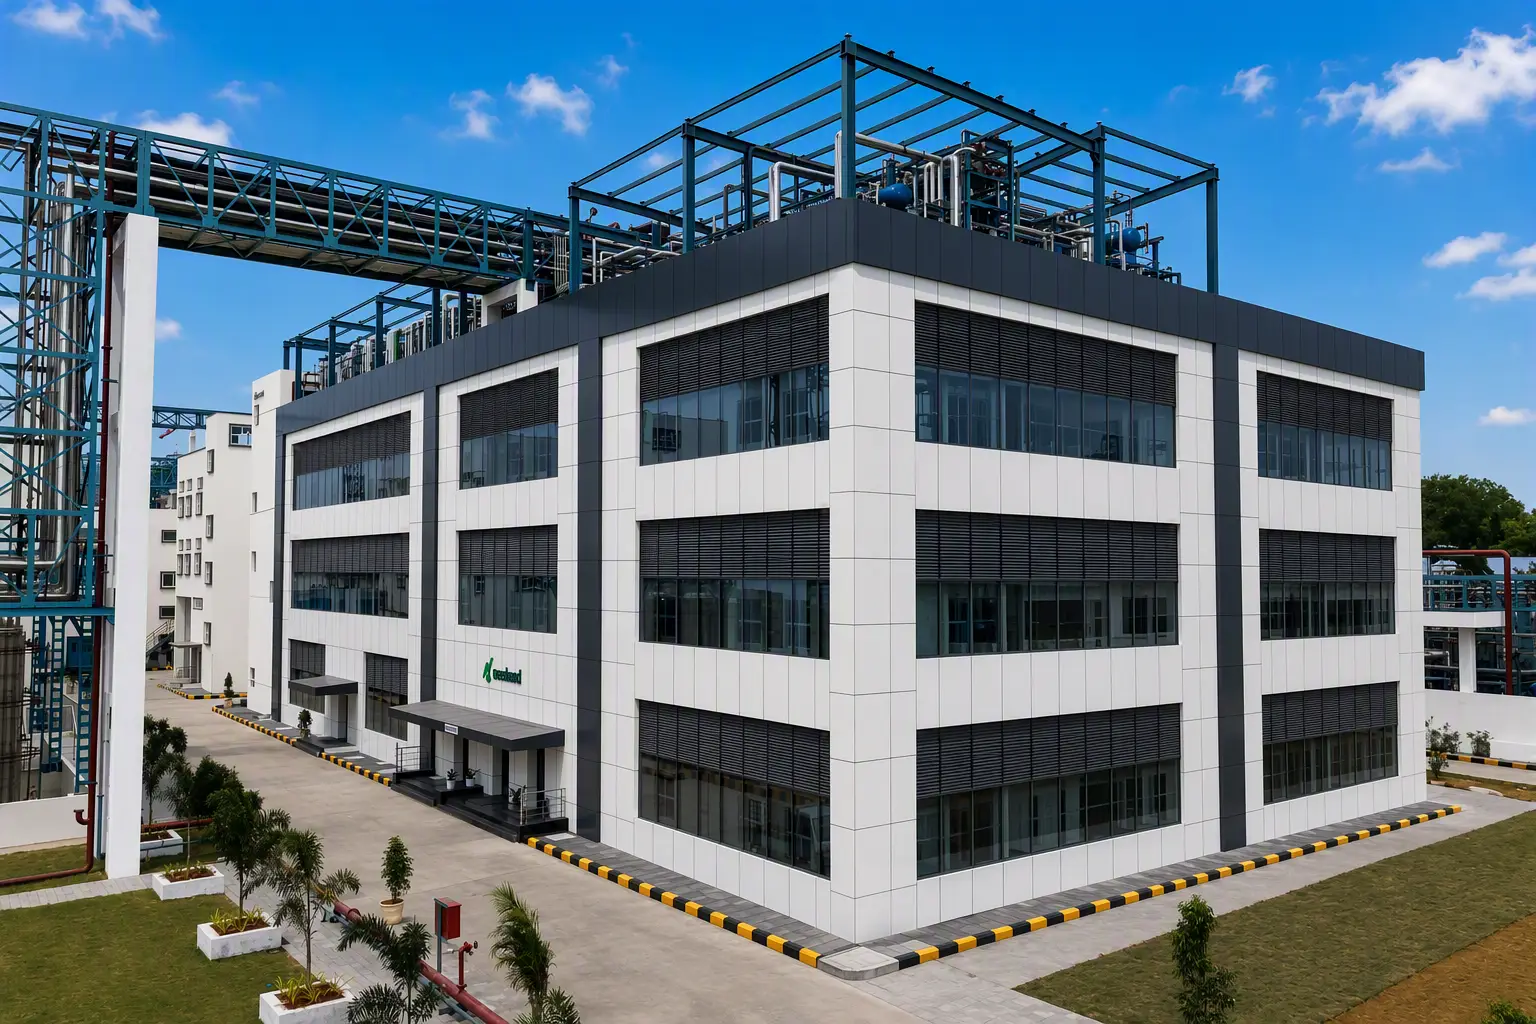
Neuland’s dedicated Peptide Manufacturing Block VI brings together automated synthesis, integrated downstream processing, advanced characterization, and GMP-ready operating systems within a purpose-built manufacturing environment in Bonthapally, Telangana.
Designed for innovators advancing complex peptide programs, the block supports SPPS, LPPS, and hybrid synthesis, with integrated purification, isolation, process analytics, and quality oversight to enable greater control from development through commercial manufacturing.
Automated through a Distributed Control System and engineered to support more than 100 kg annually, Block VI combines flexible synthesis capability, over 40 amino acid couplings, and downstream technologies such as precipitation, crystallization, spray drying, and lyophilization to strengthen process robustness and commercial manufacturability.
Block Highlights for Scalable Peptide Manufacturing
1,40,000sq ft
Purpose-built infrastructure for complex peptide development, scale-up, and commercial manufacturing
750L
Solid-phase synthesis capability to support complex peptide sequences and scale progression
6250L
Liquid-phase synthesis capability designed for larger-scale and cost-efficient peptide manufacturing
DCS-enabled automation
Enhanced process control, traceability, and operating consistency across the block
Over 100 kg/year
Built to support regulated commercial supply for peptide programs
18,000 L
Scalable infrastructure to support evolving customer demand
Integrated Capabilities for Controlled Scale-Up
Built around the capabilities customers evaluate most in peptide outsourcing: route flexibility, downstream control, robust characterization, automation, data integrity, and dependable scale-up.
Peptide Synthesis
Synthesis infrastructure supports SPPS, LPPS, and hybrid approaches, enabling route selection based on molecule complexity, scale, yield, and commercial manufacturability.1. 750 L Solid Phase Peptide Synthesis (SPPS) capacity
2. 6,250 L Liquid Phase Peptide Synthesis (LPPS) capacity
3. Hybrid synthesis capabilities
4. Global deprotection system
5. Designed for peptide fragments, complex peptides, and commercial-scale manufacturing
Purification & Isolation
Integrated purification and isolation capabilities help improve control over purity, recovery, and final form through chromatography, filtration, lyophilization, spray drying, and related technologies.1. DAC chromatography columns (1x 45 cm & 2x60 cm)
2. Tangential Flow Filtration (TFF)
3. Ion exchange chromatography
4. 100L & 200L Lyophilizers
5. Spray drying
6. Nutsche filter dryers
Process Analytics & Characterization
Advanced analytical and characterization capabilities support process development, impurity profiling, method robustness, quality control, and regulatory documentation across the peptide lifecycle.1. QTOF-HRMS
2. GC-MS
3. Circular Dichroism
4. Fluorescence Spectroscopy
5. Coulometry
6. Karl Fischer Analysis
Quality Systems Built for Regulated Supply
Quality is designed into the block through cGMP principles, electronic data integrity, segregated suites, in-process controls, and comprehensive QA/QC oversight—helping customers build confidence in regulated peptide supply without compromising operational control.1. Global cGMP design principles
2. Electronic data integrity systems
3. 21 CFR Part 11 compliance
4. Segregated manufacturing suites
5. In-process quality controls
6. Comprehensive QA/QC oversight
The Neuland Advantage in Peptide Manufacturing
Neuland combines complex-chemistry experience, dedicated peptide infrastructure, scalable GMP capability, advanced purification and analytics, automation-enabled execution, and company-wide regulatory inspection experience to support customers evaluating peptide CDMO partners.
17+ years
Experience translating complex peptide chemistry into scalable manufacturing programs~212
Peptide experts spanning chemistry, process development, analytics, quality, and manufacturing19 successful USFDA audits
Across Neuland operations, supporting customer confidence in regulated global supplyAdvance Complex Peptides with Neuland
Bring your peptide program to Neuland’s dedicated manufacturing environment—where complex-chemistry expertise, digitally enabled GMP infrastructure, integrated purification and analytics, and scalable commercial capability support the path from development to market supply.
