Meet us at CPHI Milan 2026, Booth No. 10H33, Oct 6-8, Fiera Milano, Italy Schedule a Meeting
Purpose-built for complex peptide chemistry, controlled scale-up, and reliable commercial supply.
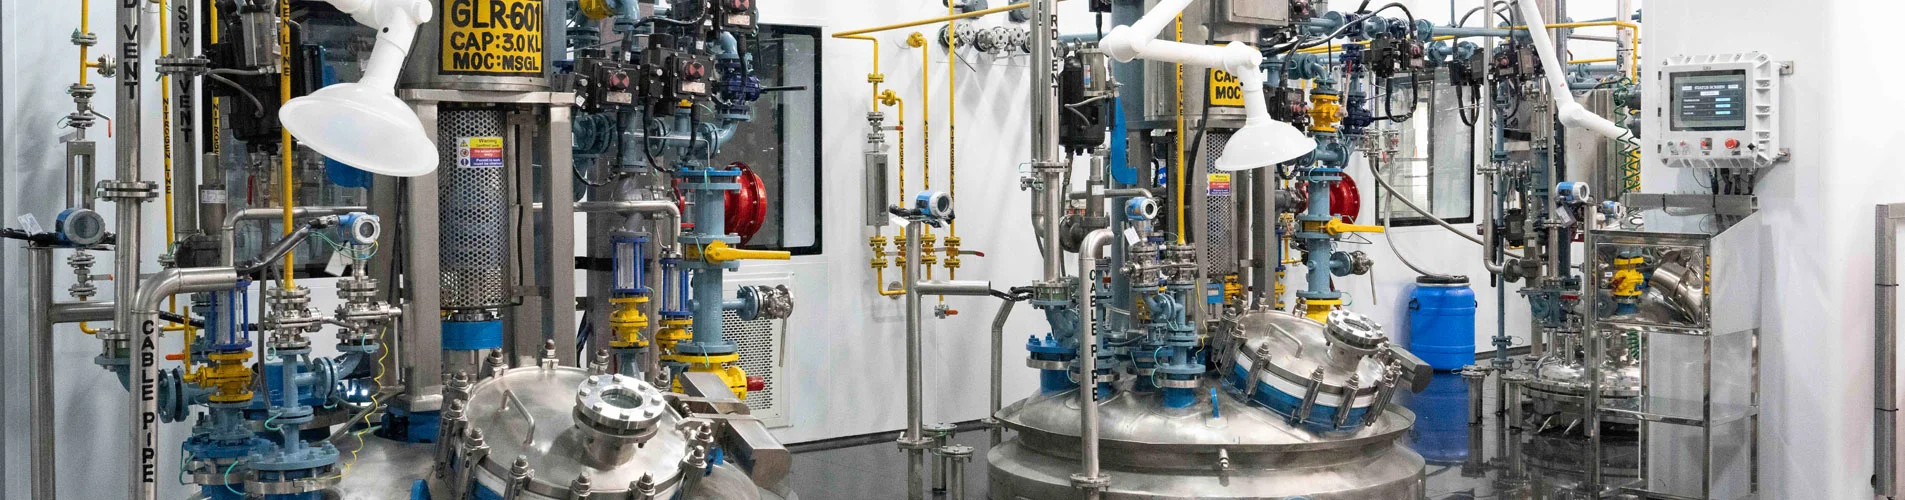
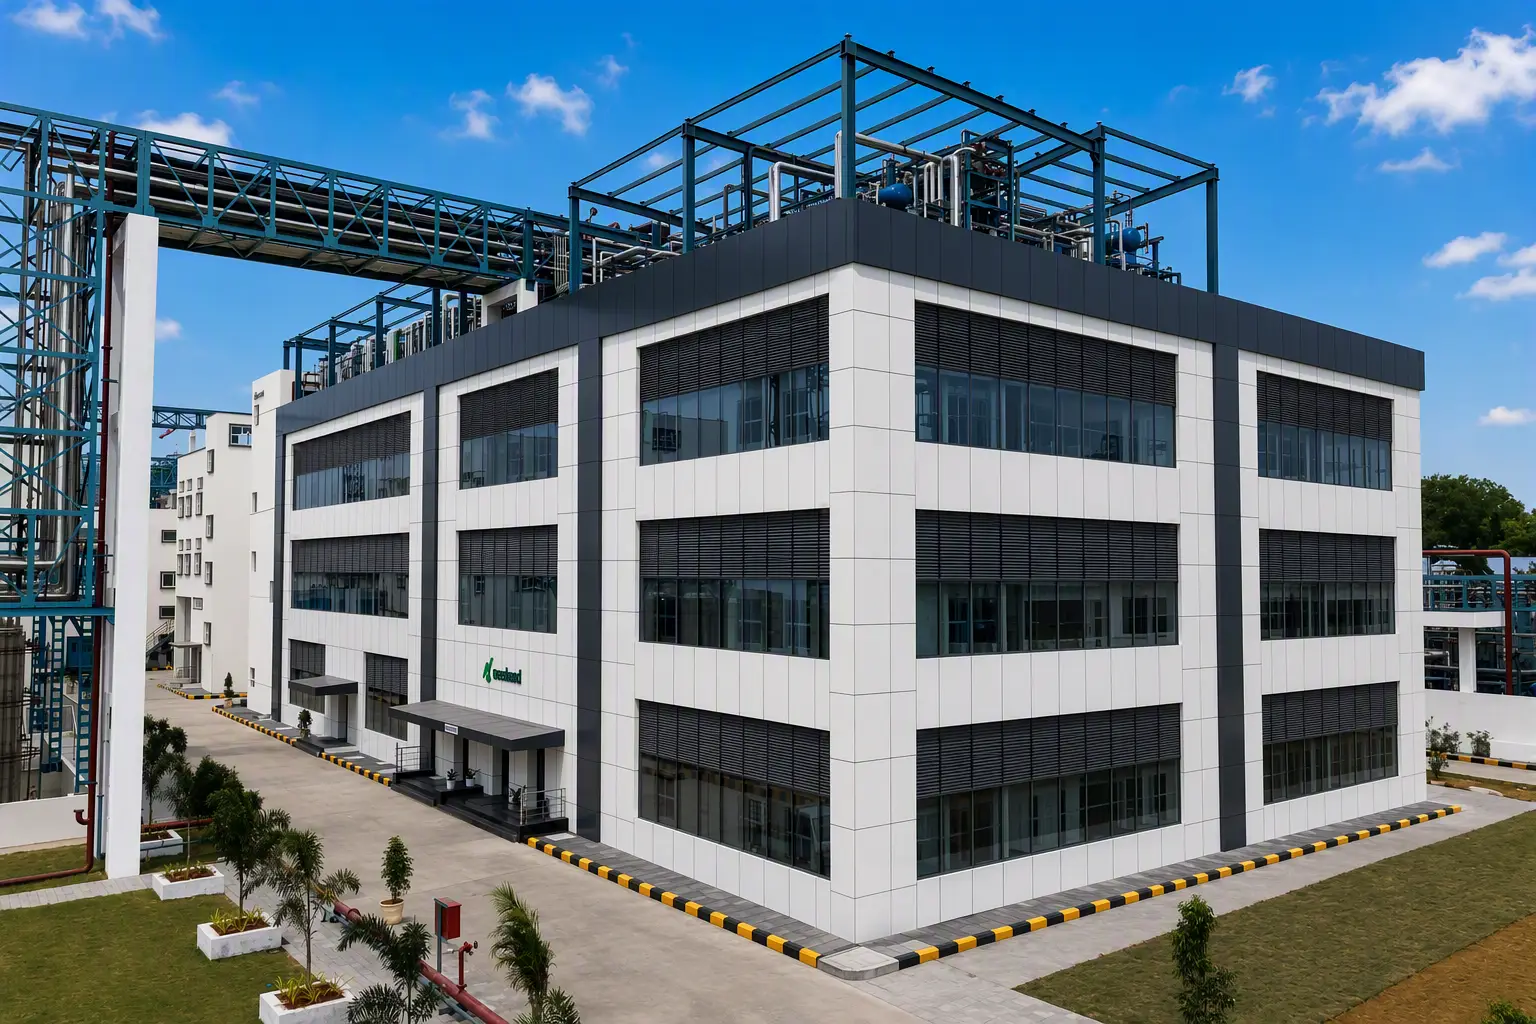
Neuland’s dedicated Peptide Manufacturing Block VI brings together automated synthesis, integrated downstream processing, advanced characterization, and GMP-ready operating systems within a purpose-built manufacturing environment in Bonthapally, Telangana.
Designed for innovators advancing complex peptide programs, the block supports SPPS, LPPS, and hybrid synthesis, with integrated purification, isolation, process analytics, and quality oversight to enable greater control from development through commercial manufacturing.
Automated through a Distributed Control System and engineered to support more than 100 kg annually, Block VI combines flexible synthesis capability, over 40 amino acid couplings, and downstream technologies such as precipitation, crystallization, spray drying, and lyophilization to strengthen process robustness and commercial manufacturability.
Neuland combines complex-chemistry experience, dedicated peptide infrastructure, scalable GMP capability, advanced purification and analytics, automation-enabled execution, and company-wide regulatory inspection experience to support customers evaluating peptide CDMO partners.
Experience translating complex peptide chemistry into scalable manufacturing programs
Cross-functional peptide expertise spanning chemistry, process development, analytics, quality, and manufacturing
Across Neuland operations, supporting customer confidence in regulated global supply
Bring your peptide program to Neuland’s dedicated manufacturing environment—where complex-chemistry expertise, digitally enabled GMP infrastructure, integrated purification and analytics, and scalable commercial capability support the path from development to market supply.
Synthesis infrastructure supports SPPS, LPPS, and hybrid approaches, enabling route selection based on molecule complexity, scale, yield, and commercial manufacturability.
Integrated purification and isolation capabilities help improve control over purity, recovery, and final form through chromatography, filtration, lyophilization, spray drying, and related technologies.
Advanced analytical and characterization capabilities support process development, impurity profiling, method robustness, quality control, and regulatory documentation across the peptide lifecycle.
Quality is designed into the block through cGMP principles, electronic data integrity, segregated suites, in-process controls, and comprehensive QA/QC oversight—helping customers build confidence in regulated peptide supply without compromising operational control.